Knowledge Base & Articles
Explore expert tips, material comparisons, structural ideas, and packaging trends to elevate your brand's unboxing experience.
Engineered B2B Secondary & High-Barrier Primary Packaging Solutions for Global Pharmaceutical, Medical Device & Biotechnology Enterprises.
Explore our top-tier packaging structural formats engineered to guarantee child-resistance, tamper-evidence, shelf-life extension, and brand authentication across global supply chains.
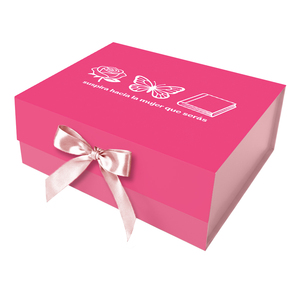
Heavy-duty structural cardboard featuring secure magnetic closures, ideal for diagnostic test kits, surgical tools, and specialty clinical drug delivery systems.
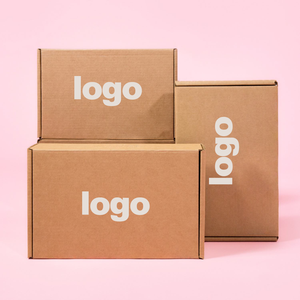
Durable, natural unbleached kraft paperboard mailer optimized for transit resistance and eco-conscious pharmaceutical direct-to-patient sampling.
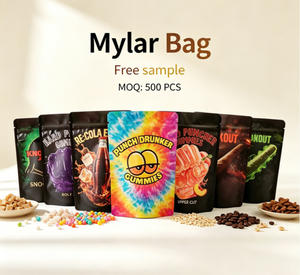
Multi-layer foil laminate pouch engineered with recloseable security zippers providing near-zero OTR/WVTR for active pharmaceutical ingredients (APIs).
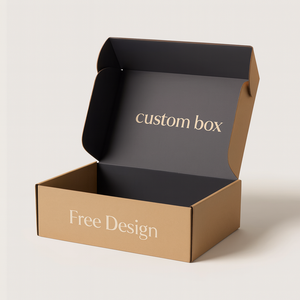
Tough rigid cardboard setup box designed for high-end OTC products, precision medical tools, and hospital supply distribution packages.
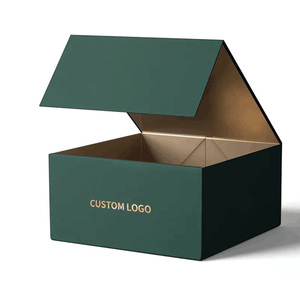
Reinforced folding rigid architecture providing structural integrity during international freight shipping for bulky medical diagnostic machinery.
Smooth, high-whiteness Solid Bleached Sulfate (SBS) paperboard folding carton engineered for high-speed automated packaging lines and crisp Braille embossing.
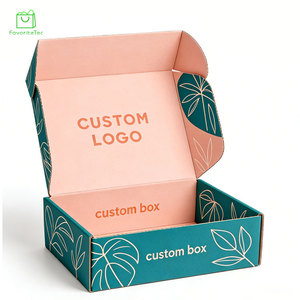
Water-resistant exterior laminate paired with precision-cut medical grade foam inserts to protect glass vials, ampoules, and pre-filled syringes during transit.
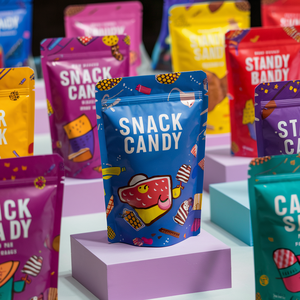
Ultra-pure barrier pouch with light-proof metalized film protecting moisture-sensitive pharmaceuticals, powders, nutraceuticals, and oral solid dosages.
An authoritative operational guide for B2B procurement managers, quality directors, and packaging engineers navigating the evolving global regulatory landscape.
The global pharmaceutical packaging ecosystem is experiencing a fundamental paradigm shift driven by stringent regulatory frameworks. Procurement officers must no longer evaluate manufacturers solely on unit economics, but on their operational capability to adhere to international traceability standards. In North America, full enforcement of the Drug Supply Chain Security Act (DSCSA) demands interoperable, electronic unit-level trace-and-track systems. Concurrently, the European Falsified Medicines Directive (EU FMD) mandates mandatory anti-tampering devices (ATDs) and unique identifiers (2D Data Matrix codes) encoded with product codes, serial numbers, lot numbers, and expiration dates.
Top-tier pharmaceutical packaging factories have integrated high-precision online vision verification systems directly into folding carton lines. This ensures that every primary blister pack, secondary folding box, and tertiary shipping carton exhibits 100% error-free variable data printing. Packaging designs must now seamlessly accommodate serialization zones without sacrificing structural integrity or brand real estate.
Key Takeaway for B2B Purchasing Officers: Ensure your contract packaging manufacturer maintains certified cGMP cleanrooms (ISO 15378 standard), provides full material batch traceability, and guarantees 2D Data Matrix print durability against abrasion, moisture, and extreme cold-chain temperatures.
Engineered safety remains a cornerstone of pharmaceutical packaging design. Under ISO 8317 and US ASTM D3475 standards, secondary packaging and recloseable flexible pouches must satisfy demanding Child-Resistant and Senior-Friendly (CRSF) protocols. The industry's primary technical challenge lies in balancing child impediment (preventing over 80-85% of children under 5 years from accessing contents within a 5-minute test period) with effortless accessibility for senior patients aged 50 to 70 suffering from dexterity limitations or arthritis.
Modern structural innovations utilize dual-push-and-slide lock mechanisms, squeeze-and-turn notches, and hidden release buttons integrated into rigid cardboard sleeves and flexible barrier laminates. Leading factories employ automated CAD dieline engineering to test tactile feedback prior to mass production, significantly lowering validation lead times for pharmaceutical OEMs.
Global environmental mandates and corporate ESG objectives are compelling pharmaceutical manufacturers to phase out non-recyclable multi-material plastics and toxic per- and polyfluoroalkyl substances (PFAS). Traditional high-barrier blisters reliant on PVDC coatings are rapidly being replaced by recyclable mono-material polyolefin films, high-density FSC-certified SBS paperboards, and water-based barrier dispersions.
For secondary packaging, top factories are pioneering 100% plastic-free folding cartons fabricated with post-consumer recycled (PCR) fiber and printed using non-toxic, vegetable-based inks. These sustainable substrates maintain equal bursting strength, compression resistance, and moisture protection while reducing the corporate carbon footprint by up to 42%.
With the global market expansion of biologic drugs, mRNA vaccines, cell-and-gene therapies, and injectable insulins, maintaining temperature stability between 2°C to 8°C (and down to -80°C for ultra-cold formulations) is paramount. Smart pharmaceutical packaging now incorporates active IoT temperature data loggers, time-temperature indicators (TTIs), and contactless NFC tags directly into secondary box walls.
Procurement teams are prioritizing manufacturers capable of engineering custom vacuum insulation panels (VIPs), phase change material (PCM) cavities, and shock-absorbing molded pulp or EVA foam cradles. This integrated approach shields delicate parenteral glass vials from thermal excursion and mechanical vibration during transcontinental air freight.
Selecting the appropriate substrate requires evaluating Water Vapor Transmission Rate (WVTR), Oxygen Transmission Rate (OTR), light protection, and structural rigidity.
| Material Grade | Primary Structure | WVTR / OTR Protection | Regulatory Compliance | Optimal Pharmaceutical Application |
|---|---|---|---|---|
| SBS Paperboard (300-400gsm) | Solid Bleached Sulfate Virgin Fiber | Medium (Requires Barrier Coating) | FDA 21 CFR Compliant | Secondary Prescription Boxes, OTC Folding Cartons |
| Alu-Alu Foil (CFF) | Cold-Formed OPA / Aluminum / PVC | Ultra-High (Near Zero Barrier) | USP Class VI / EP Standard | Hygroscopic Tablets, Capsules, Highly Sensitive APIs |
| PET/AL/PE Laminate Pouch | Multi-Layer Foil Matrix with Zip | High Light & Moisture Shielding | CRSF Certified (ISO 8317) | Oral Powders, Reagents, Diagnostic Test Pouches |
| 1200gsm Rigid Chipboard | High-Density Recycled Fiberboard | High Structural Compression Strength | FSC Certified Board | Surgical Equipment Cases, High-Value Biologic Kits |
| E/B-Flute Corrugated Board | Fluted Kraft Wall Linerboard | High Impact Drop Protection | ISTA 3A Transit Tested | Clinical Trial Direct Mailers, Cold-Chain Shippers |
Incorporating void-indicator tapes, fiber-tear paper seals, and micro-perforated tear strips ensuring immediate visual verification of uncompromised drug integrity.
Fully compliant with Marburg Medium Braille standards for visually impaired patient safety, flawlessly executed via high-speed rotary embossing dies.
CAD-customized anti-static EVA, IXPE foam, or recyclable molded paper pulp inserts engineered to lock vials, ampoules, and syringes firmly in place.
Leveraging advanced manufacturing infrastructure to streamline pharmaceutical packaging procurement from structural CAD dieline creation to mass delivery.
Unlike legacy packaging converters that impose heavy upfront tooling fees, our modern digital setup and automated die-cutting workflows eliminate die and plate charges entirely. Whether you require a short-run validation batch of 100 boxes for clinical trials or a commercial run of 500,000 units, we provide flexible low minimum order quantities (MOQs) with full cost transparency.
Accelerate your drug development approval timelines with our in-house packaging design team. We offer complimentary 3D digital mockups and precision structural dielines within 24 hours. Physical unprinted structural prototypes or fully printed proof samples are produced rapidly so your quality team can conduct drop tests and physical fit checks before full line production.
Our primary and secondary production facilities operate under ISO 15378 certified quality management systems specifically designed for primary packaging materials for medicinal products. Cleanroom environments, automated HEPA air filtration, pest-proof barrier control, and strict hygiene protocols guarantee zero micro-contamination during printing, die-cutting, and gluing.
Time-to-market is critical in pharmaceutical drug launches. Upon final digital artwork proof approval, commercial production is completed within 7 to 10 business days. Supported by our global logistics network, we deliver door-to-door air and sea freight across the United States, Europe, and Asia-Pacific with complete customs clearance assistance.
Direct expert answers to technical, regulatory, ordering, and manufacturing questions frequently raised by B2B pharmaceutical buyers.
Partner with an industry-leading packaging manufacturer trusted by global pharmaceutical enterprises. Get instant engineering support, free 3D dieline proofs, and competitive factory-direct wholesale pricing.
Get Catalog