ISO 15378 & FDA Title 21 CFR Compliant Packaging

Custom Pharmaceutical
Packaging Boxes

Precision-engineered, tamper-evident, and child-resistant pharmaceutical packaging boxes designed for prescription drugs, OTC medicines, medical devices, and biologics. Guaranteed quality compliance, track-and-trace serialization, and low-migration inks.

ISO 15378 Certified Production Tamper-Evident & Child-Resistant DSCSA Serialization Ready
Cleanroom ManufacturingISO Class 8 capable facilities
Braille & Tactile EmbossingEN 15823 European compliance
Anti-CounterfeitingMicro-text, IR inks & holograms
Wholesale AgilityLow 100 MOQ to multi-million runs

Technical Procurement Primer

Engineering Compliance in Custom Pharmaceutical Packaging Boxes

Navigating global drug safety mandates, barrier science, and structural integrity for prescription and over-the-counter pharmaceutical products.

In the highly regulated pharmaceutical supply chain, secondary packaging serves as far more than an outer shell. Custom Pharmaceutical Packaging Boxes represent a critical defense layer designed to safeguard drug potency, ensure patient adherence, prevent illicit tampering, and satisfy strict statutory guidelines enforced by the US FDA, European Medicines Agency (EMA), and global health authorities. For procurement managers, packaging engineers, and contract manufacturing organizations (CMOs), selecting the correct packaging supplier requires rigorous evaluation of substrate purity, barrier efficacy, and anti-counterfeiting integration.

Hello Custom Boxes manufactures high-performance pharmaceutical folding cartons and rigid packaging solutions under strict ISO 15378 quality standards (Primary and Secondary Packaging Materials for Medicinal Products). By combining low-migration food-and-drug grade inks with automated vision-inspection systems, we eliminate contamination risks while delivering 100% dimensional accuracy compatible with ultra-high-speed cartoning equipment such as Uhlmann, Bosch/Syntegon, and Marchesini.

Key Regulatory & Technical Mandates Covered:

  • FDA 21 CFR Part 211: cGMP Packaging & Labeling Controls
  • ISO 21976:2020: Tamper Verification Features for Packaging
  • 16 CFR § 1700.20: Child-Resistant Testing Specifications
  • EN 15823: Packaging Braille Requirements for Medical Cartons
  • DSCSA Compliance: 2D DataMatrix Serialization & Traceability
  • FSC & PEFC Certification: Sustainable Virgin Fiber Board Sourcing

Structural Portfolio

Recommended Box Styles for Pharmaceutical Applications

Tailored structural designs optimized for blister packs, pill bottles, liquid vials, ampoules, diagnostic kits, and medical devices.

01
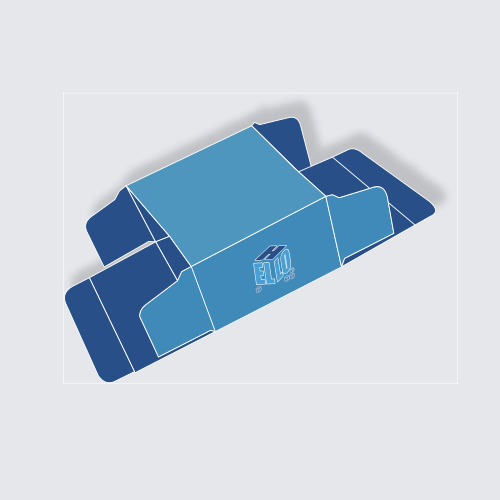
Reverse Tuck End Pharmaceutical Box Dieline

Reverse Tuck End (RTE) Pharma Cartons

The industry gold standard for unit-dose blister packaging, ointment tubes, and small pill bottles. Features compact footprints, quick manual or automated assembly, and clean presentation surfaces.

Standard Substrate
14pt - 18pt SBS Paperboard
Security Feature
Tamper-Evident Stickers / Void Tape
Compliance
EN 15823 Braille Ready

Best for: OTC oral solids, topical creams, blister packs
02
Straight Tuck End Medical Box Dieline

Straight Tuck End (STE) Window Cartons

Constructed with top and bottom tuck flaps closing to the rear, preserving a pristine front display panel. Frequently engineered with clear PET die-cut windows for product visibility.

Standard Substrate
16pt - 24pt Bleached Board
Security Feature
Custom Holographic Void Seals
Compliance
FDA Direct Food/Drug Contact

Best for: Cough syrups, diagnostic test kits, eye drops

03
Auto Bottom Pharmaceutical Display Box Dieline

Auto-Lock Bottom Heavy-Duty Cartons

Engineered with an interconnected self-locking base that instantly snaps open. Capable of supporting heavy liquid glass bottles, IV bags, and bulk pharmaceutical containers without bottom failure.

Standard Substrate
20pt - 28pt SBS / E-Flute
Security Feature
Reinforced Structural Locks
Compliance
Drop-Test ASTM D5276 Certified

Best for: Heavy liquid bottles, bulk syrups, parenteral solutions

04
Child-Resistant Lock Box Dieline

Child-Resistant (CR) Push-Lock Boxes

Specially engineered with patented internal locking tabs and squeeze-and-slide release mechanisms. Prevents access by young children while remaining senior-friendly for prescription therapies.

Standard Substrate
Laminated High-Density Board
Security Feature
Internal Dual Locking Tabs
Compliance
16 CFR § 1700.20 Protocol

Best for: Controlled substances, potent therapeutics, pediatric risks

05
Sleeve and Tray Ampoule Box Template

Sleeve & Rigid Insert Vial Boxes

Two-piece sliding drawer and sleeve boxes equipped with custom-molded pulp or high-density foam inserts to lock delicate glass ampoules and vaccine vials rigidly in place during transit.

Standard Substrate
Rigid Setup Board + Poly Foam
Security Feature
Vibration & Shock Absorption
Compliance
Cold Chain ISTA 7E Ready

Best for: Biologics, injectable vials, clinical drug trials

06
Partition Box for Medical Supplies

Partitioned Shipping & Distribution Cartons

Custom corrugated outer shippers featuring internal cell dividers (fence partitions). Prevents glass-to-glass contact and breakage across long-distance freight and international distribution routes.

Standard Substrate
B-Flute / C-Flute Corrugated
Security Feature
Impact & Crush Resistance
Compliance
UN 3373 Medical Sample Spec

Best for: Multi-pack distribution, clinical samples, lab reagents

Require a custom structural dieline or engineered sample for your pharmaceutical product?

Send an Inquiry

Engineering Specifications

Material Selection & Barrier Science

Comparing medical-grade board stocks, protective coatings, and anti-counterfeiting printing options for pharmaceutical packaging.

Board Substrate Caliper / Grammage Barrier Performance Print Surface Quality Recommended Applications
Solid Bleached Sulfate (SBS) 14pt - 24pt (280 - 450 gsm) Moderate UV protection; high moisture resistance with dispersion coatings. Superior white brightness (90+ ISO); optimal for fine text & 2D barcodes. Ethical drugs, prescription solids, clinical trials, retail OTC packaging.
Unbleached Kraft Board 16pt - 28pt (300 - 500 gsm) High tear strength & puncture resistance; organic moisture barrier. Natural brown, matte tactile surface; best for minimalist/eco branding. Herbal remedies, botanical supplements, eco-conscious healthcare.
Micro-Flute Corrugated (E/F Flute) 1.2mm - 1.6mm thickness High crush resistance & thermal insulation for cold-chain packs. Direct offset printing or litho-laminated high gloss/matte sheets. Diagnostic machinery, bulk ampoule transport, e-commerce pharmacy shipping.
Rigid Greyboard (Wrapped) 1.5mm - 3.0mm thickness Maximum structural rigidity, impact shielding, and long-term shelf stability. Wrapped in specialty coated papers with foil stamping, spot UV, or embossing. High-value biologics, luxury medical devices, physician sample kits.
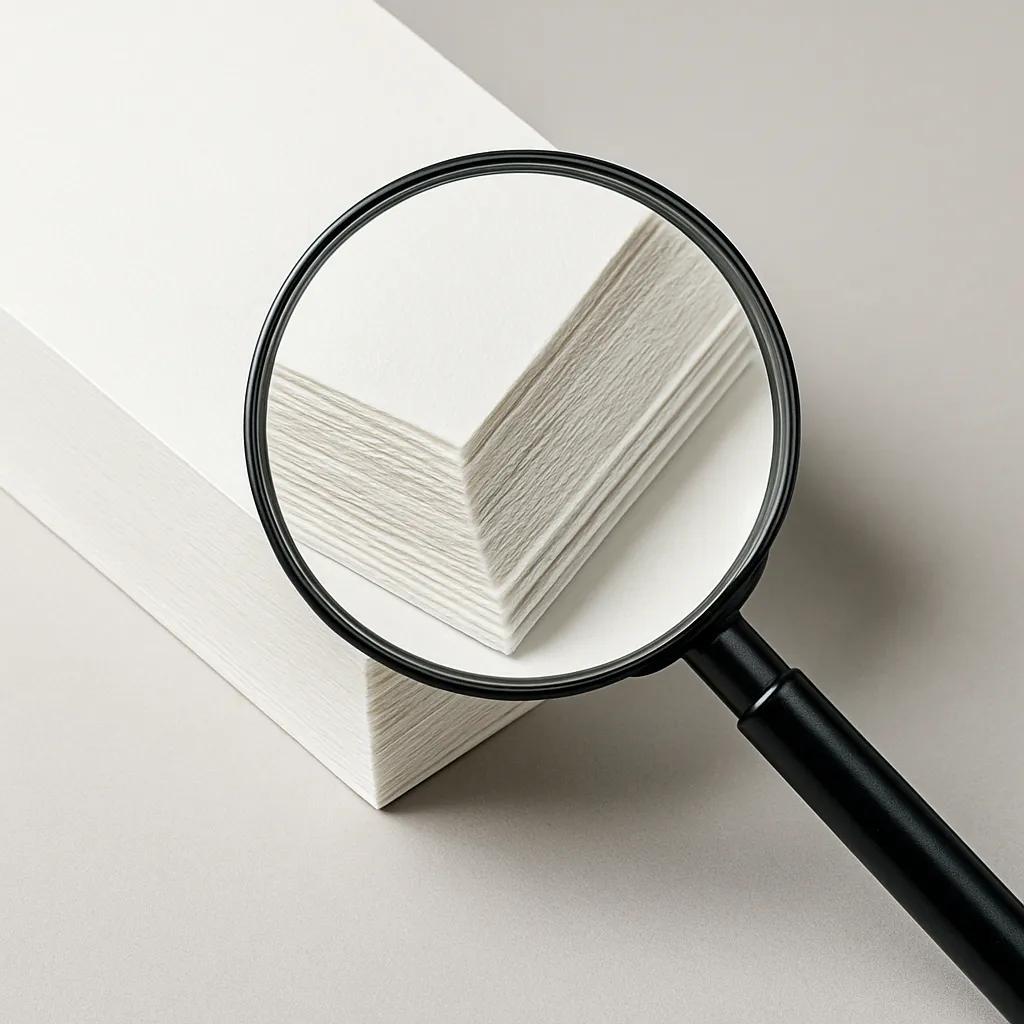
Medical Grade SBS Board for Pharmaceutical Packaging

Medical-Grade SBS Board

100% virgin wood pulp board manufactured without optical brighteners. Pure white, smooth surface ensuring flawless scan rates for GS1 2D DataMatrix codes and braille dot consistency.

Compliance: FDA Title 21 CFR 176.170 compliant for direct & indirect contact.

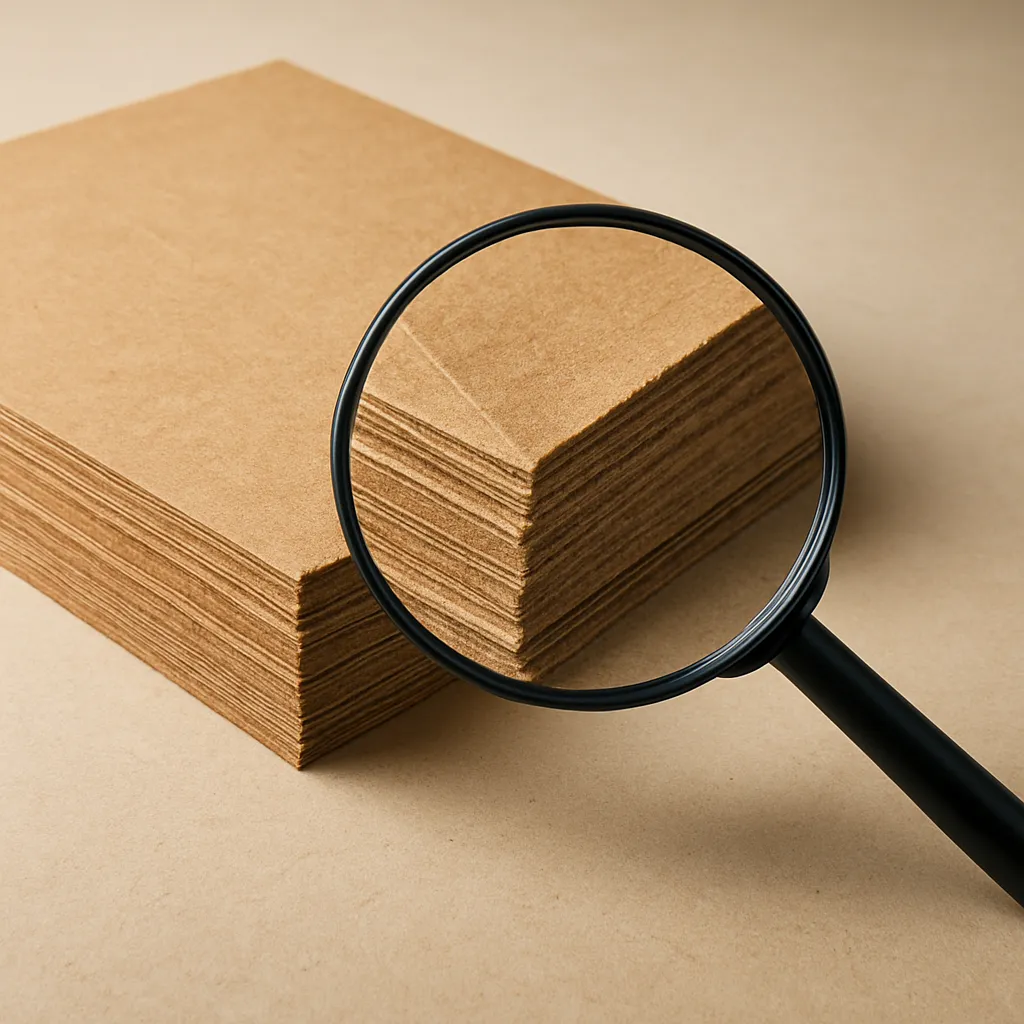
Recyclable Kraft Paperboard for Natural Medicine

Recyclable Unbleached Kraft

Ultra-durable virgin fiber board ideal for eco-friendly pharmaceutical brands seeking carbon footprint reduction without compromising burst strength or structural protection.

Sustainability: 100% Biodegradable, FSC-certified forest sourcing.

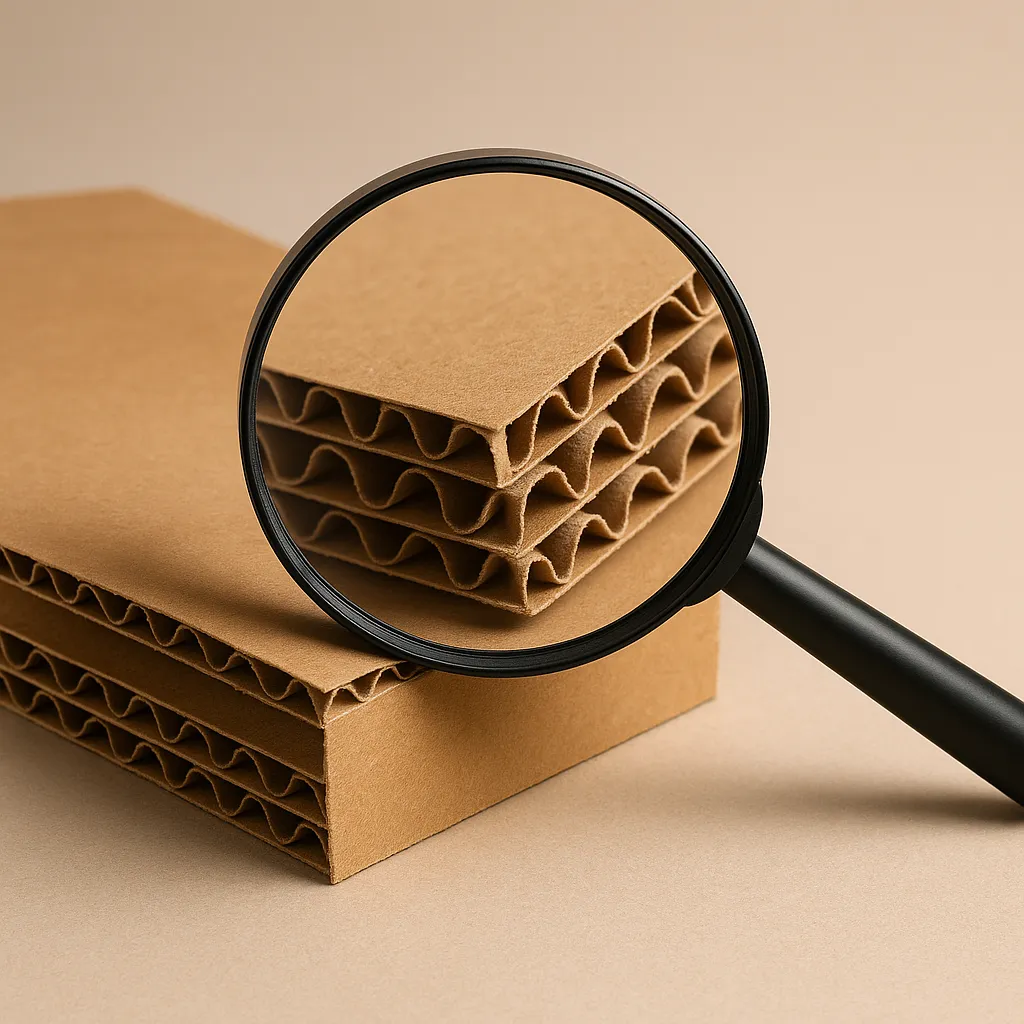
Insulated Corrugated Shipper for Vaccine Distribution

Insulated Corrugated Board

Fluted structural board engineered for thermal protection and secondary shock absorption during freight transit. Compatible with gel packs and temperature indicators.

Application: Cold-chain biologics, clinical trial supply shipping.

Enterprise Capability

Why Leading Pharma Brands Partner With Hello Custom Boxes

Built on technical expertise, cleanroom quality standards, zero-defect quality control, and global supply chain elasticity.

ISO 15378 Compliance

Manufactured under strict GMP guidelines ensuring zero cross-contamination and complete batch traceability.

Vision-System Quality Assurance

100% automated optical camera inspection verifying barcode legibility, print registration, and color tolerance (Delta E < 1.0).

Low-Migration Inks

Formulated strictly with vegetable-based, solvent-free inks complying with Swiss Ordinance and Nestlé guidance for zero chemical leaching.

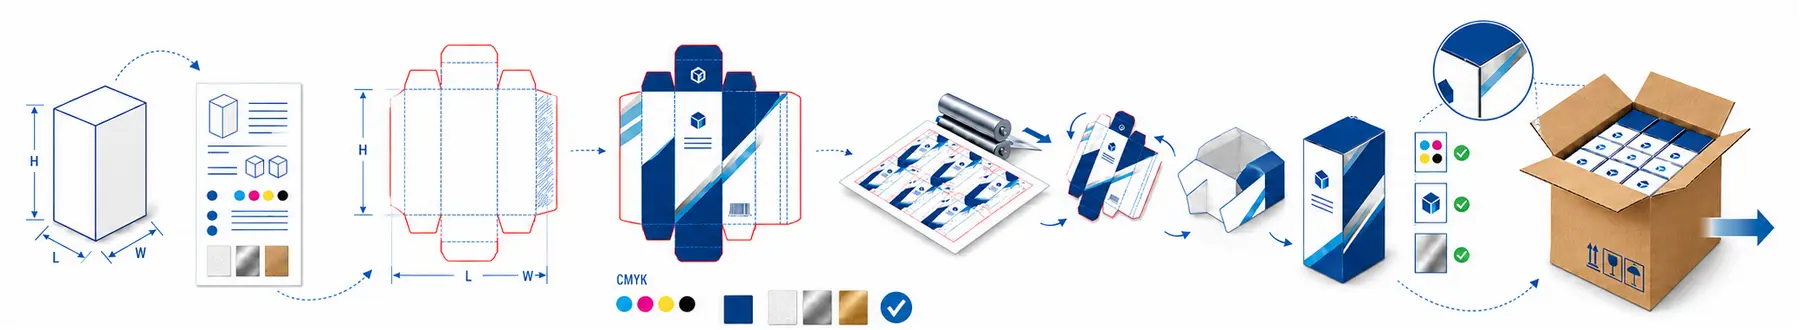
24-Hour CAD Dieline Proofing

Rapid 3D structural rendering and physical sample production to validate automated packaging line compatibility.

Elastic Supply Chain

Scalable production from 100 boxes for clinical trials to millions of units with guaranteed fast USA & international delivery.

High-speed automated pharmaceutical packaging line and quality inspection facility

Ready to Audit Our Quality Systems or Request a Quotation?

Connect directly with our senior pharmaceutical packaging engineers. We provide comprehensive compliance documentation, material safety data sheets (MSDS), and press-proof samples.

Send an Inquiry

Procurement Knowledgebase

Custom Pharmaceutical Packaging Boxes FAQ

Detailed technical answers to common questions asked by pharmaceutical buyers, quality assurance officers, and packaging engineers.

Our custom pharmaceutical packaging boxes are engineered and manufactured in facilities operating under ISO 15378 guidelines (Primary and Secondary Packaging Materials for Medicinal Products) and ISO 9001 quality management systems. We ensure compliance with FDA Title 21 CFR Part 211 cGMP regulations for labeling and packaging control. Structural capabilities include child-resistant testing under 16 CFR § 1700.20, European blind accessibility standards via EN 15823 Braille embossing, and tamper-verification features conforming to ISO 21976:2020.

Tamper-evident secondary packaging prevents unrecorded access to medicinal products. We integrate multiple tamper-verification mechanisms, including: 1) Special tear-strip structures integrated into the carton flaps that permanently destroy the board upon opening; 2) Frangible adhesive void labels that leave irreversible text indicators ("VOID" or "OPENED") if unsealed; and 3) Custom glued tuck flap closures requiring structural tearing to access the primary blister pack or bottle.

To eliminate volatile organic compound (VOC) transfer and chemical leaching, we exclusively utilize 100% virgin Solid Bleached Sulfate (SBS) paperboards certified free of optical brighteners. All printing is executed using low-migration, low-odor, vegetable oil-based offset inks and water-based aqueous coatings formulated according to the Swiss Ordinance list and EuPIA (European Printing Ink Association) guidelines for food and drug safety.

Yes. Our inline digital and hybrid printing presses are equipped with high-resolution continuous inkjet and thermal inkjet systems capable of printing variable GS1-compliant 2D DataMatrix barcodes, National Drug Code (NDC) identifiers, unique serial numbers, lot codes, and expiration dates at high speeds. Every printed code undergoes 100% automated optical verification to guarantee Grade A/B scan legibility under ANSI/ISO grading standards.

We supply a multi-tiered security defense portfolio. Overt security options include custom 2D/3D holographic foils, color-shifting optic inks, and serial tamper-evident seals. Covert security options include micro-printed text (invisible to the naked eye), UV-fluorescent invisible inks, infrared-absorbing pigments, and hidden taggants within aqueous coatings readable only via specialized field detectors.

Absolutley. We precision die-cut all folding cartons with dimensional tolerances held within ±0.5mm. Flap scorelines, pre-broken side seams (typically 180° pre-fold), and glue tab geometry are specifically engineered to eliminate jamming and ensure flawless feed rates on automated high-speed packaging lines including Uhlmann, Bosch/Syntegon, Marchesini, and CAM cartoners.

To support agile pharmaceutical development, clinical trials, and niche orphan drug launches, our minimum order quantity starts at just 100 boxes. For commercial-scale pharmaceutical distribution, our automated high-volume production lines cost-effectively scale to hundreds of thousands or millions of units per month.

You can request precise Adobe Illustrator vector dielines by clicking the "Send an Inquiry" button and providing your primary container dimensions (bottle diameter/height, blister card dimensions, or vial pack count). We generate 2D CAD dielines within 24 hours and can dispatch unprinted physical structural prototypes for fit testing prior to final production approval.