Industry Expertise & Manufacturing Insights
Comprehensive Guide to Custom Food Packaging Procurement
Selecting the optimal food packaging supplier is a critical strategic decision for restaurant chains, commercial bakeries, packaged food distributors, and food service importers worldwide. Food containers must perform flawlessly under physical stress, variable temperatures, moisture exposure, and grease migration while strictly maintaining compliance with global food safety regulations.
1. Defining Structural Integrity & Food-Grade Compliance
When engineering custom food boxes, direct food contact requires certified raw materials. Paperboard surfaces coming into contact with food items must be free from harmful chemicals, heavy metals, and non-food-safe recycled fibers. At Hello Custom Boxes, our primary packaging substrates utilize virgin wood fibers sourced from FSC-certified mills, coupled with soy-based or water-based flexographic and offset inks.
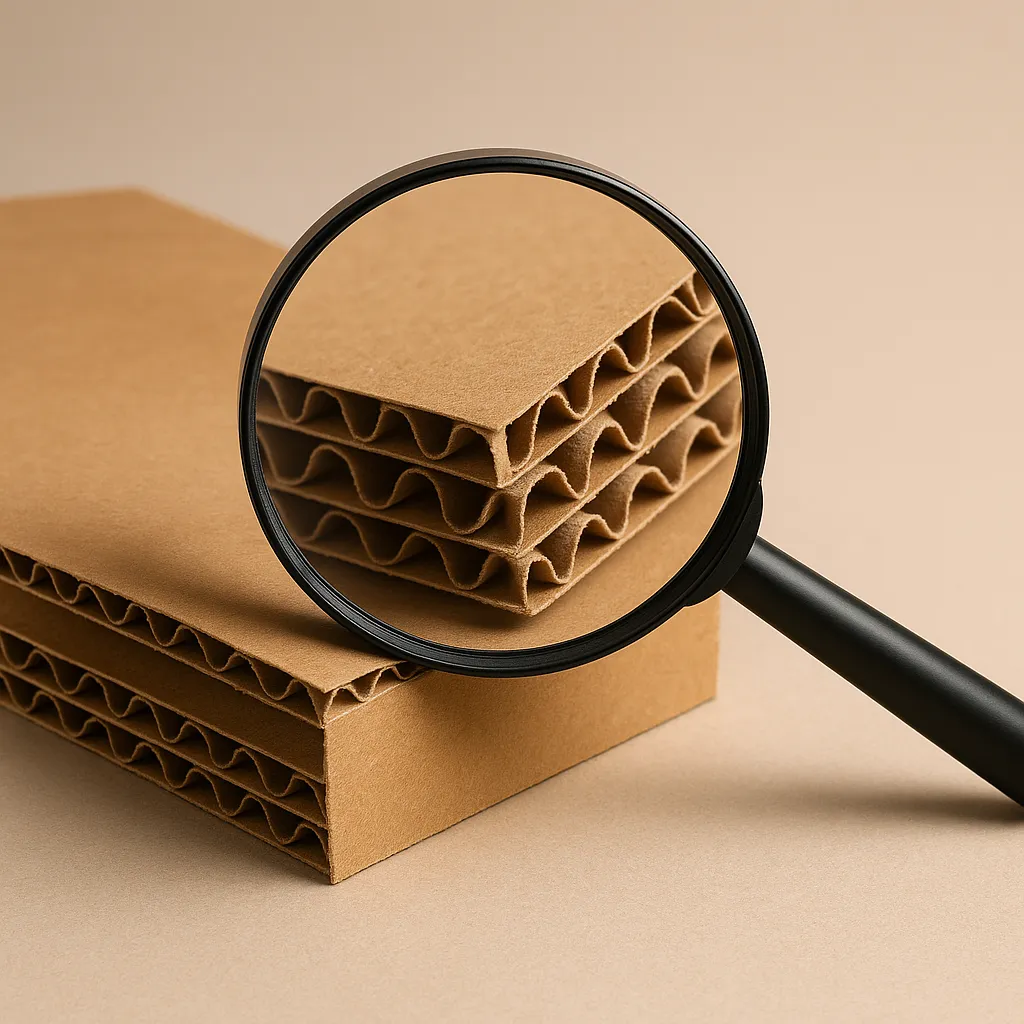
Structural stability must also account for stacking compression strength during logistics. For heavy or bulk food products, micro-flute corrugated structures provide exceptional crush resistance while keeping overall package weight low to optimize international freight expenditures.
2. Grease Resistance, Barrier Liners & Moisture Control
Uncoated paperboard absorbs oil, steam, and moisture rapidly, compromising the physical box structure and staining brand graphics. To counter this, specialized barrier coatings are applied during manufacturing:
- Kit-Rated Oil Resistance: Surface treatments measured from Kit 1 to Kit 12 designed to repel animal fats, vegetable oils, and hot grease.
- Aqueous Barrier Coatings: Eco-friendly, water-based coatings that provide moisture and oil protection while keeping paperboard 100% repulpable and recyclable.
- Polyethylene (PE/2PE) Liners: Extruded film barriers essential for frozen food storage, preventing freezer burn, carton softening, and condensation damage.
- Venting Engineering: Strategic die-cut steam release vents integrated into hot takeaway boxes to prevent fried foods from becoming soggy during delivery transit.
3. B2B Inventory Optimization & Flat-Packed Logistics
Warehouse space management is a primary operational concern for large food service operations. All our folding carton designs—including reverse tuck end, auto-bottom, and snap-lock structures—are engineered to ship flat. Pre-glued auto-bottom cartons reduce assembly time by up to 70% at the kitchen packing station, ensuring rapid throughput during peak service hours.
4. High-Impact Customization & Retail Brand Differentiation
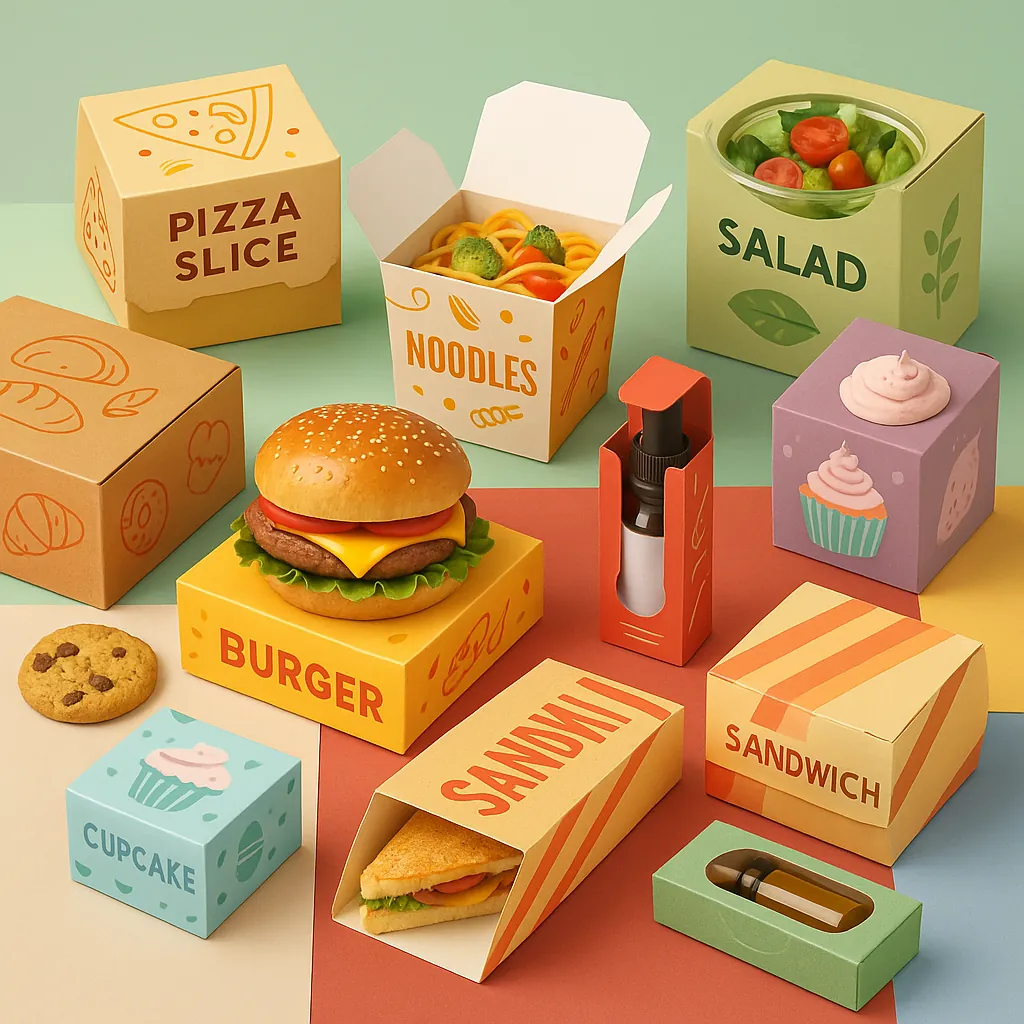
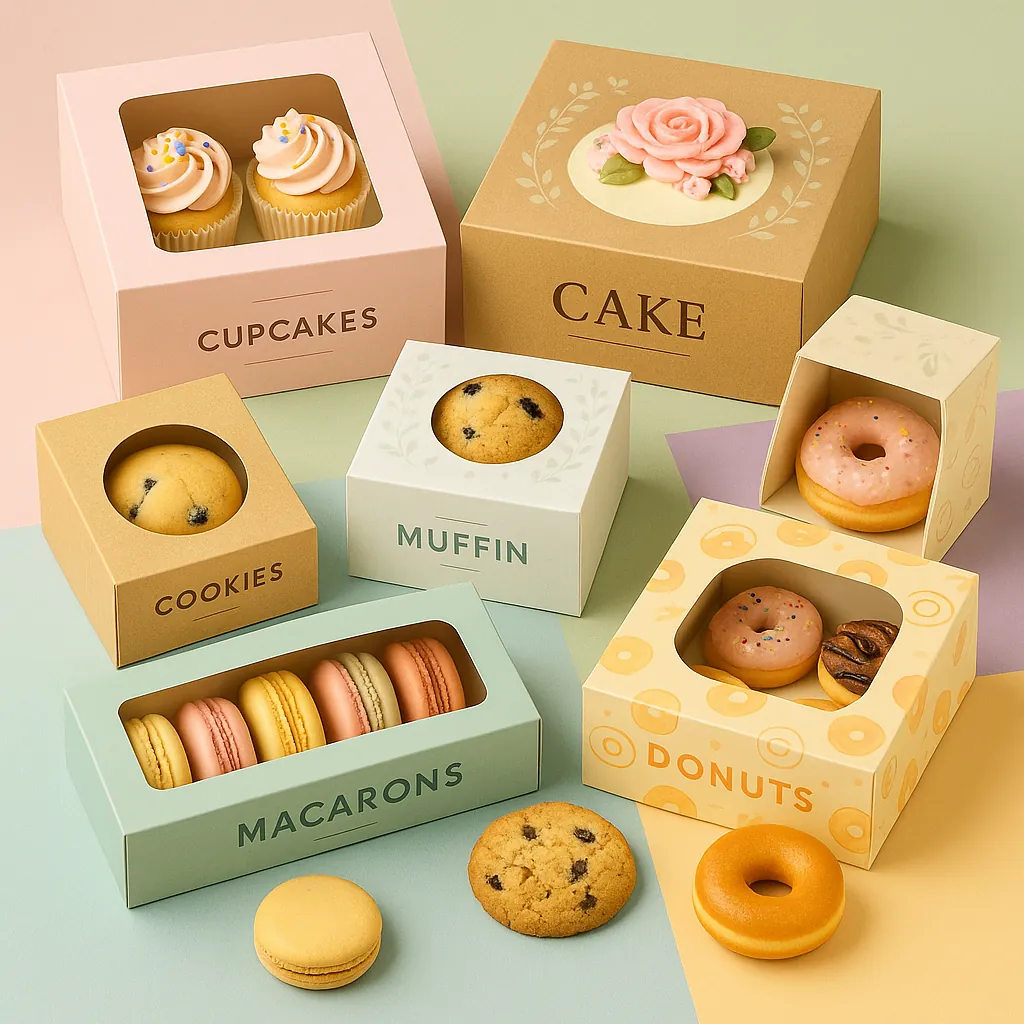
Food packaging is often the primary visual touchpoint for your brand. Advanced CMYK offset printing combined with Pantone spot color precision guarantees absolute brand color consistency across multiple production batches. Premium finishes such as spot UV highlights, foil stamping, soft-touch lamination, and custom window die-cuts elevate retail presence and build buyer trust on competitive store shelves.