Knowledge Base & Articles
Explore expert tips, material comparisons, structural ideas, and packaging trends to elevate your brand's unboxing experience.
Explore our precision-engineered pharmaceutical boxes and barrier pouches, customized for biomedical manufacturers, OTC exporters, and medical device innovators across Aichi Prefecture.
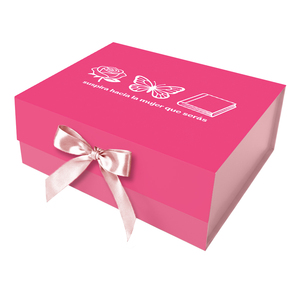
Heavy-duty rigid cardboard with magnetic closure. Ideal for premium medical presentation kits, surgical instruments, and high-value drug sample distribution.
Contact Us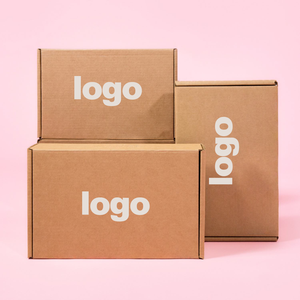
Recyclable unbleached Kraft corrugated paperboard designed for eco-conscious pharmaceutical direct-to-patient (DTP) shipping and clinical supply logistics.
Contact Us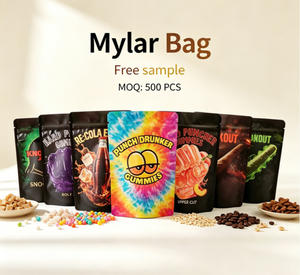
Multi-layer PET/AL/PE foil pouch offering near-zero oxygen and moisture permeability. Engineered for moisture-sensitive active pharmaceutical ingredients (APIs).
Contact Us
Precision structural rigid packaging with customized interior dimensions. Perfect for clinical trial diagnostics, healthcare consumables, and OTC branding.
Contact Us
Space-saving foldable design that snaps into a rigid box. Cuts freight costs to Central Japan International Airport while maintaining luxury unboxing aesthetics.
Contact Us
High-density SBS paperboard with protective aqueous varnish. Engineered for tamper-evident secondary packaging in retail pharmaceutical chains.
Contact Us
Water-resistant laminated surface equipped with custom-cut high-density EVA foam / sponge insert. Built for liquid vials, glass ampoules, and fragile medical sensors.
Contact Us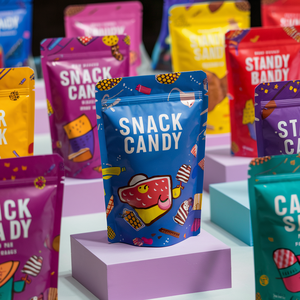
Matte-finished laminated foil pouch with child-resistant (CR) zip seal options. Suitable for granular dosage forms, nutraceuticals, and medical powders.
Contact UsUnderstanding regulatory alignment, thermal insulation requirements, and supply chain dynamics across the Chubu economic region.
Nagoya serves as the central operational hub for the Chubu economic zone, bridging biopharmaceutical innovation from Aichi Prefecture, Mie, and Gifu. With major research clusters surrounding Nagoya University, Obu City Health Plaza, and biomedical industrial parks in Kariya, pharmaceutical procurement managers demand packaging suppliers capable of strict structural consistency and zero-contaminant production.
Japan’s Pharmaceuticals and Medical Devices Agency (PMDA) imposes stringent compliance parameters on drug distribution. Secondary folding cartons must pass rigorous JIS Z 0200 packaging performance standards, ensuring anti-burst strength during highway transit along the Ise-Wangan and Tomei Expressways.
Under Japan's updated Resource Circulation Strategy for Plastics, pharmaceutical distributors in Nagoya are rapidly substituting single-use petroleum plastics with high-performance FSC-certified Solid Bleached Sulfate (SBS) paperboard, water-based barrier coatings, and biodegradable film laminations.
Selecting the right paperboard substrate and barrier film matrix for moisture-sensitive active compounds, biologics, and medical devices.
| Packaging Material Class | Grammage / Thickness Range | WVTR (Water Vapor Transmission Rate) | Primary Industrial Application in Nagoya | Compliance & Test Standard |
|---|---|---|---|---|
| Virgin SBS Paperboard | 300 GSM – 450 GSM (16pt - 24pt) | Standard Varnish (15-20 g/m²/day) | Secondary OTC Cartons, Prescription Pill Boxes | JIS P 8124 / ISO 5636 |
| Aqueous Coated Barrier Board | 350 GSM – 500 GSM | High Barrier (< 2.5 g/m²/day) | Moisture-Sensitive Tablets, Diagnostic Test Strip Boxes | ASTM E96 Water Vapor Test |
| PET/AL/PE Foil Laminate | 70 µm – 130 µm Film Gauge | Ultra Barrier (< 0.05 g/m²/day) | API Powders, Granules, Reagent Pouches | ISO 15106-2 Infra-red Sensor |
| E-Flute Corrugated Board | 1.5 mm Flute (350g Kraft/120g Medium) | Structural Shock Barrier | Clinical Trial Sample Mailers, Biologic Vials Shippers | JIS Z 0401 / ECT 32 Cushion Test |
| Rigid Greyboard + EVA Foam | 1200 GSM Board + Custom Foam density | Impact Absorption & Physical Protection | Surgical Instrument Kits, Endoscopic Equipment Boxes | ISO 2248 Drop Test Standard |
Need custom laboratory validation reports or physical prototype testing before mass production?
How our factory solves real-world packaging challenges for biomedical exporters, clinical packaging teams, and OTC distributors across Chubu.
Biologics dispatched via Central Japan International Airport (Centrair) require rigid outer cartons that withstand condensation inside insulated cold-chain shippers (+2°C to +8°C). Our custom waterproof-laminated mailer boxes with high-density EVA sponge inserts keep glass vials immobilized during flight turbulence and customs clearance.
Nagoya’s major drugstore supply networks require retail-ready boxes equipped with irreversible structural void-locks or perfs. When a consumer opens the carton, security tabs snap visibly, fulfilling both Japanese Ministry of Health guidelines and consumer safety expectations without needing external plastic shrink wrap.
For medical device manufacturers in Kariya and Toyota City producing diagnostic devices and lab reagents, we manufacture custom magnetic rigid boxes featuring multi-tier compartments. Each component (pipette, reagent pouch, sensor) sits flush in anti-static ESD foam inserts.
Streamlining the procurement pipeline from original structural CAD dielines to international customs delivery.
Eliminate design errors before tooling. We provide zero-cost 3D digital renderings and precise vector dieline templates compatible with Adobe Illustrator within 24 hours of receiving your product dimensions.
Lower your upfront capital expenditure. Whether ordering 100 sample units for clinical trials or 100,000 commercial batch boxes, we absorb structural die-cutting die setup costs to optimize your packaging ROI.
Every printed box passes through inline high-speed CCD camera sensors, inspecting color delta-E variations, registration misalignments, and dust contamination under strict GMP Class 100,000 cleanroom standards.
Direct technical and commercial answers regarding lead times, PMDA standards, custom sampling, and regional freight logistics.
Yes. Our pharmaceutical secondary packaging boxes are produced in ISO 15378 certified manufacturing lines. Materials are tested for burst resistance, ink migration, and light-shielding properties in alignment with PMDA guidelines and Japanese Industrial Standards (JIS Z 0200). We can provide Certificate of Analysis (CoA) documentation for raw paperboard and food-safe aqueous coatings upon request.
Standard production takes 7 to 10 business days following artwork proof approval. Air express freight directly into Central Japan International Airport (Centrair - NGO) takes approximately 3 to 5 days. For bulk container freight destined for the Port of Nagoya (Meiko), ocean transit typically averages 7 to 12 days, ensuring rapid door-to-door delivery across Aichi Prefecture.
Absolutely. We support low Minimum Order Quantities (MOQ starting at 100 pieces for folding cartons and rigid magnetic boxes). This enables biopharmaceutical startups around Nagoya University and clinical trial teams to conduct pilot studies without tying up capital in excessive inventory.
Yes. Our high-resolution industrial printing systems support high-density GS1-128 and GS1 DataMatrix 2D codes. We guarantee Grade A/B barcode scannability (ISO/IEC 15415) to ensure seamless integration with pharmaceutical inventory tracking systems throughout Japan's wholesale and hospital supply chains.
All bulk export shipments are vacuum-sealed inside heavy-duty moisture-barrier polybags containing industrial silica gel desiccant packs before being packed into reinforced 5-ply double-wall outer corrugated shipping cartons. Cartons are fully stretch-wrapped on wooden or plastic pallets for ultimate moisture and shock protection during marine transit.
Yes. We provide both unprinted plain structural samples (to verify exact dimensional fit with your bottles, blisters, or devices) and fully printed production-grade prototypes. Samples can be dispatched via international courier directly to your office or facility in Greater Nagoya within 3 to 5 business days.