Knowledge Base & Articles
Explore expert tips, material comparisons, structural ideas, and packaging trends to elevate your brand's unboxing experience.
Engineered for Malaysian pharmaceutical manufacturers, contract packagers (CMOs), and medical device exporters requiring strict moisture barrier protection, tamper evidence, and brand distinction.
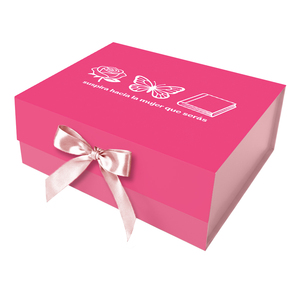
Rigid foldable cardboard with magnetic closure. Ideal for premium surgical kits, clinical trial supplies, and diagnostic presentation boxes.
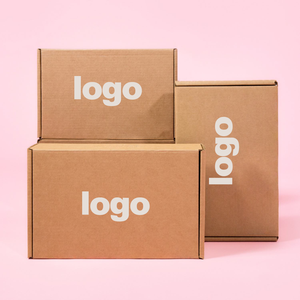
Durable, recyclable corrugated kraft mailers designed for e-pharmacy dispatch, herbal supplements, and cold-chain transit secondary protection.
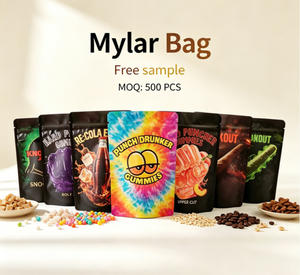
Multi-layer aluminium foil interior with moisture-proof zip seal. Essential protection for active pharmaceutical ingredients and oral powders.
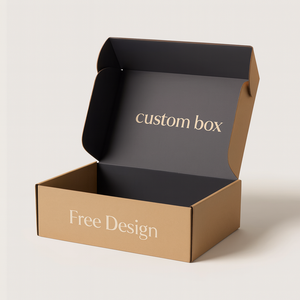
Heavy-duty rigid cardboard presentation boxes with custom printed lid. Suited for hospital delivery packs and premium pharmaceutical samples.
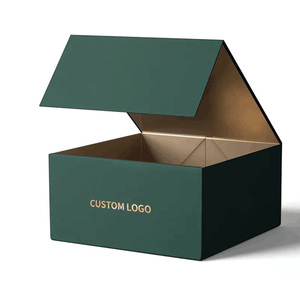
Space-saving collapsible rigid structure with strong magnet locking. Engineered for specialized therapeutics, injectable devices, and diagnostics.
High-speed machine-insertable paperboard cartons. Precision die-cut for oral solid dosage blister packs, syrups, and topical creams.
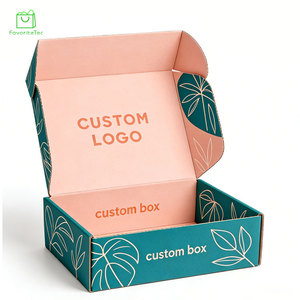
Embossed protective box with precision shock-absorbing EVA foam lining. Protects sensitive glass vials and liquid diagnostic reagents during export.
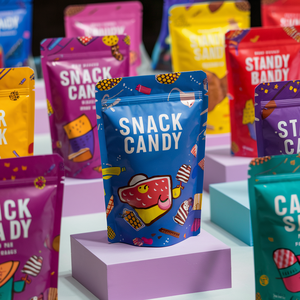
Custom printed aluminium barrier pouches with tear notches and ziplocks. Maximum protection against light, oxygen, and high humidity.
Malaysia stands as one of the most dynamic pharmaceutical markets within the ASEAN alliance, driven by rigorous regulatory frameworks established by the National Pharmaceutical Regulatory Agency (NPRA) under the Ministry of Health Malaysia (Kementerian Kesihatan Malaysia). For pharmaceutical manufacturers, generic distributors, and contract manufacturing organizations (CMOs) exporting into or operating within Malaysia, packaging is far more than a structural container—it is a critical control point for product efficacy, patient safety, and regulatory compliance under the Quest3+ registration system.
A primary challenge for pharmaceutical packaging in Malaysia is climatic endurance. Under the International Council for Harmonisation (ICH) stability testing guidelines, Malaysia is classified under Zone IVb (Hot & Very Humid: 30°C ± 2°C / 75% RH ± 5% RH). Standard packaging substrates imported from temperate regions frequently fail in this extreme environment, suffering from moisture vapor ingress, delamination, seal degradation, and compromised structural integrity during storage and transit across Port Klang and Penang Port hubs.
Furthermore, Malaysia's unique status as a global hub for Halal-certified pharmaceuticals (under standard MS 2424: General Guidelines for Halal Pharmaceuticals) dictates that all packaging substrates, coatings, printing inks, and adhesives must be certified non-contaminated, free from animal-derived additives, and processed under strict hygienic conditions aligned with Good Manufacturing Practice (GMP).
Tailored packaging solutions configured to meet the distinct operational demands of Malaysia's primary healthcare manufacturing and logistics zones.
Serving the high-density Bayan Lepas Free Industrial Zone and Kulim Hi-Tech Park. We provide custom waterproof embossed mailer boxes with precision EVA shock-absorbing foam inserts for sterile diagnostic kits, surgical tools, and glass vial exports.
Supporting major generic drug packagers across Shah Alam, Petaling Jaya, and Rawang. Supplying high-speed machine-insertable SBS folding cartons, tamper-evident blister tuck boxes, and auto-bottom cartons optimized for automated secondary packaging lines.
Delivering temperature-stable secondary packaging for cold-chain biologics and insulin products moving between Singapore and Iskandar Malaysia. Multi-layer corrugated shipping cartons equipped with thermal insulation barriers.
Choosing the appropriate packaging substrate and barrier configuration is essential to prevent product recalls caused by humidity-induced clumping, active degradation, or packaging collapse. Below is our engineered technical matrix designed specifically for export into tropical Southeast Asian regions.
| Packaging Category | Material Composition | Barrier Capabilities | NPRA / Industry Application |
|---|---|---|---|
| Barrier Folding Cartons | SBS (Solid Bleached Sulfate) + PE/Alu Lamination (250–400 gsm) | High resistance to MVTR; smooth printing surface for 2D matrix serialization | Oral Solid Dosage (OSD) blisters, OTC medicine boxes, topical creams |
| Resealable Mylar Pouches | PET / VMPET / LLDPE or PET / ALU / PE (70–150 microns) | Zero light transmission; MVTR < 0.01 g/m²/day; high puncture resistance | Active Pharmaceutical Ingredients (APIs), nutraceutical powders, diagnostic test strips |
| Rigid Magnetic Display Boxes | 1200–1800 gsm Greyboard wrapped in 157 gsm Art Paper + Soft Touch Matte Lamination | Extreme crush resistance; tamper-evident magnetic closure seals | Medical device presentation, hospital drug launch kits, high-value biologic therapies |
| Cold-Chain Shipper Mailers | 3-ply E/B Flute Corrugated Board + Water-Repellent Outer Sizing Coating | High bursting strength; stack resistance under humidity; thermal reflection | Secondary shipper box for refrigerated vaccines, diagnostic reagents, e-pharmacy logistics |
Strategic insights for procurement directors and brand owners preparing for regulatory shifts and technological advancements in ASEAN markets.
With NPRA aligning closer to international PIC/S guidelines, serialization via high-density 2D DataMatrix barcodes, GS1 standards, and anti-tamper security seals is becoming essential. Our ultra-smooth SBS paperboard substrates support high-speed variable inkjet printing with zero bleed.
Malaysia's leadership in Halal pharmaceuticals (MS 2424) requires packaging exporters to guarantee full supply chain traceability. All raw paper pulps, synthetic coatings, and press inks are documented animal-free to prevent cross-contamination for global Islamic export markets.
In response to Malaysia's Roadmap Towards Zero Single-Use Plastics 2018–2030, pharmaceutical procurement officers are replacing traditional plastic blister outer cartons with 100% recyclable biodegradable paperboard folding boxes treated with bio-based water-repellent coatings.
As a specialized pharmaceutical packaging exporter, we bridge the gap between rigorous scientific compliance and agile, cost-effective manufacturing. We understand that packaging delays directly impact drug launch timelines and batch approvals.
Technical and operational answers for procurement officers, quality assurance managers, and regulatory affairs specialists in Malaysia.
Yes. Our pharmaceutical-grade substrates—including coated SBS paperboard and barrier foil laminations—are engineered and tested to maintain MVTR and structural integrity under Zone IVb conditions (30°C / 75% RH). We provide technical data sheets (TDS) and material certificates for your NPRA registration dossiers.
Absolutely. We ensure that all paper pulps, barrier films, coatings, press inks, and adhesives are 100% free from pork derivatives, animal fats, or alcohol contaminants. Full raw material traceability documentation can be provided to support your JAKIM / Halal certification audits.
Yes. We offer both unprinted structural samples (plain white/kraft prototypes) to test dimensional fit with your primary containers and fully printed pre-production proofs to evaluate color accuracy, foil stamping finish, and barcode readability.
We integrate multiple anti-counterfeit measures into our custom folding boxes, including custom hologram foil stamping, void-tamper seals, micro-text printing, UV fluorescent inks, and precision-printed 2D DataMatrix serial numbers for track-and-trace systems.
Once your final artwork is verified, manufacturing takes 7 to 10 business days. Transit time via air freight to KLIA takes approximately 3 to 5 days, while ocean freight shipments to Port Klang or Penang Port typically take 12 to 18 days depending on the shipping line.
Our minimum order quantity starts at just 100 units for standard custom printed folding cartons and rigid magnetic boxes, making us an ideal partner for clinical trial packaging, product launch testing, as well as full-scale commercial distribution.
Consult with our packaging technical specialists to receive custom structural dielines, 3D mockups, and competitive wholesale factory quotes engineered for NPRA compliance.